Processing Defects of Hostaform POM and Solutions - 1
What is Hostaform POM?
1. Warpage and Dimensional Distortion
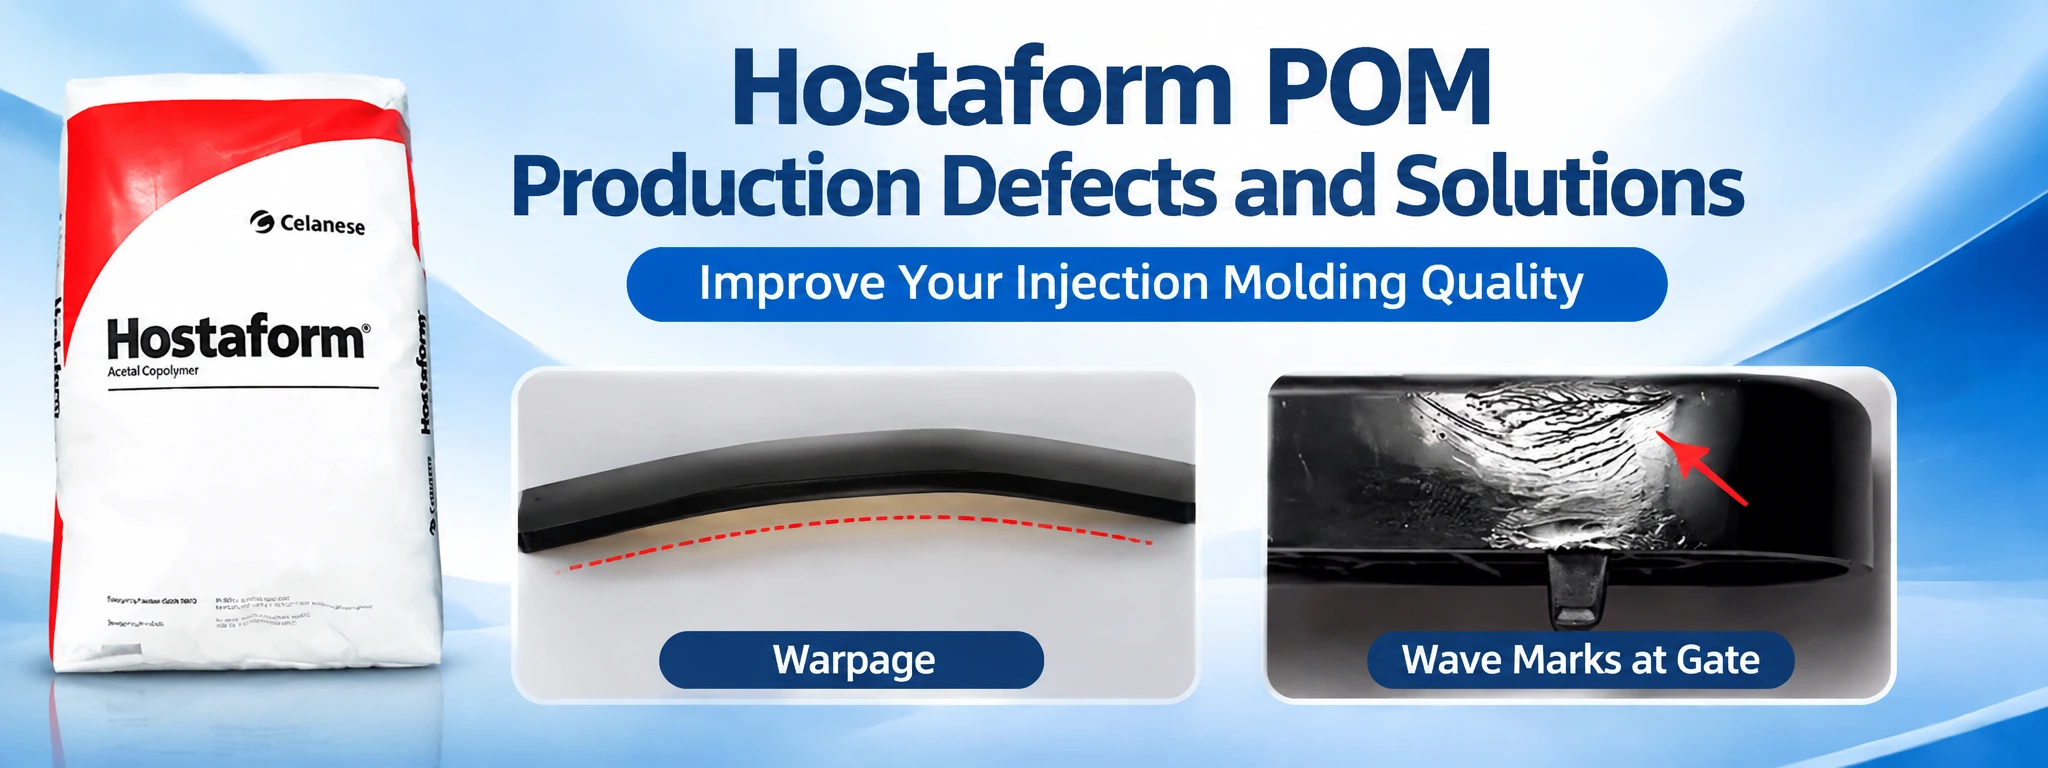
Warpage is an extremely common processing defect in the injection molding of Hostaform POM, causing the product to exhibit noticeable warping and dimensional shrinkage after demolding.
The cause of this problem is as follows: Hostaform POM is a highly crystalline engineering plastic. Differences in cooling rates between various parts of the product—such as thick-walled and thin-walled sections—create internal stress, which ultimately leads to warping. This phenomenon is commonly observed in long, flat, and thick-walled products.
Proposed Solution

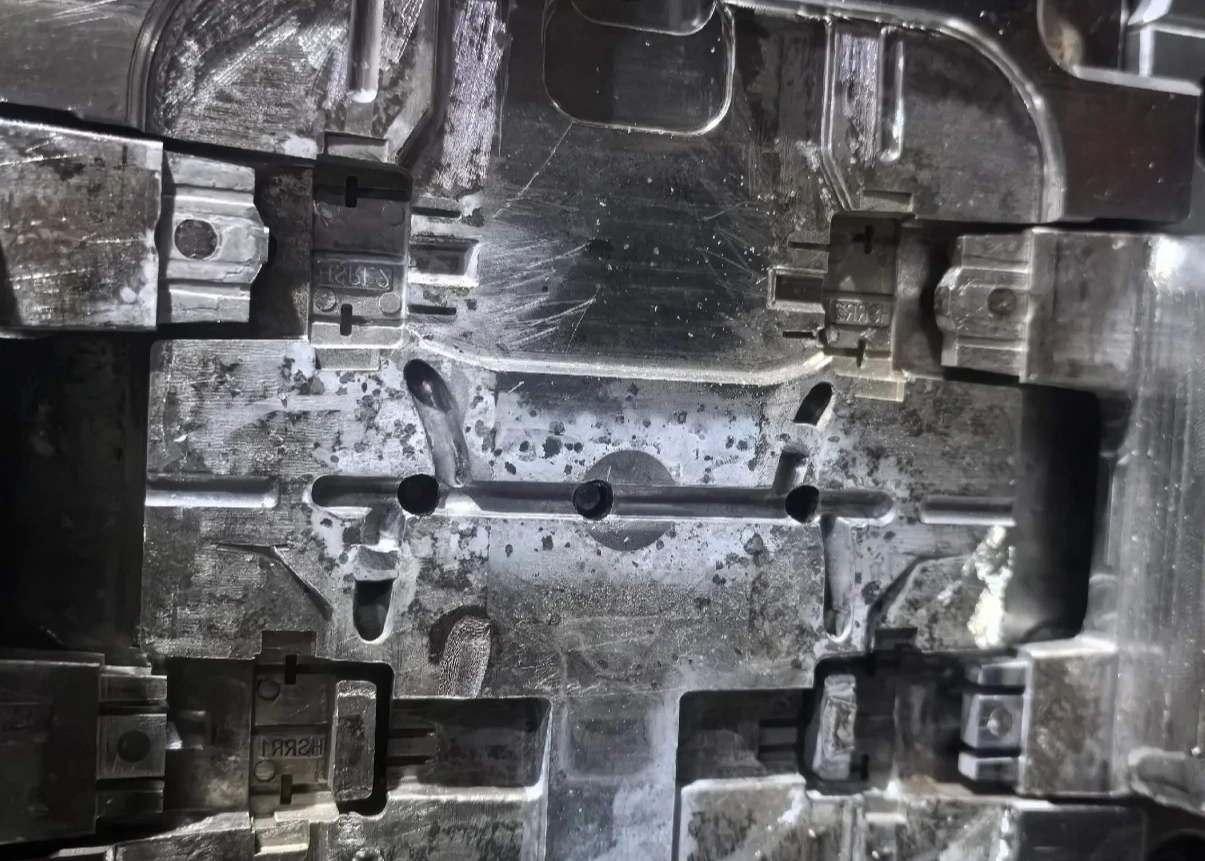
2. The mold has turned white and has charred residue on it
This is a serious processing defect caused primarily by the formation of formic acid—a byproduct resulting from the reaction between formaldehyde released during the decomposition of Hostaform POM material and oxygen—due to localized overheating of polyoxymethylene (POM) during processing.
This defect is commonly seen when using raw materials of lower purity, as the presence of other materials can cause POM to degrade. We recommend using Hostaform POM C, which offers better temperature resistance
| Hostaform C 9021 | Hengli HLM90 | Yuntianhua Yuncon M90 | |
| Heat deflection temperature 1.8 MPa | 104℃ | 85℃ | 95℃ |
| Vicat softening temperature | 150℃ | - | - |
Initially, polyformaldehyde products—commonly seen as white or light-colored precipitates, as shown in the figure on the right—can interfere with the product’s venting and demolding; subsequently, formic acid is produced, which is a moderately corrosive substance that can corrode metal molds.
Proposed Solution
1. Lower the barrel temperature to prevent thermal degradation of Hostaform POM material caused by melt temperatures exceeding the recommended range.
2. Reduce the dwell time of Hostaform POM material in the mold
3. Clean the mold promptly to prevent localized material degradation caused by residual material.
4. Check for malfunctions in the temperature control system; older equipment is prone to thermocouple and monitoring system malfunctions.
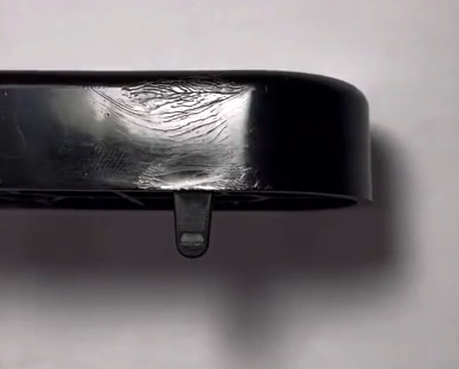
3. Wavy Patterns at the Injection Nozzle
The cause of waviness at the gate location in Hosatform POM products is still due to the high crystallinity of the POM material itself, which leads to material buildup caused by inconsistent cooling rates. This defect primarily occurs at the gate and at the bottom of the gate. There are various causes for this issue, and the following points should be systematically investigated:
1. The injection gate is too small, resulting in excessively high shear rates as the Hostaform POM melt passes through the gate.
2. Melt ejection caused by excessive injection speed
3. Localized cooling caused by a mismatch between the recommended melt temperature for Hostaform POM and the mold temperature
Why ABS is commonly used in electroplated application